Visual inspection.
Defined checks and records.
Use controlled lighting, fixtures and selected vision checks to support product inspection.
Discuss this capabilityApplication-dependent development · Proposed capability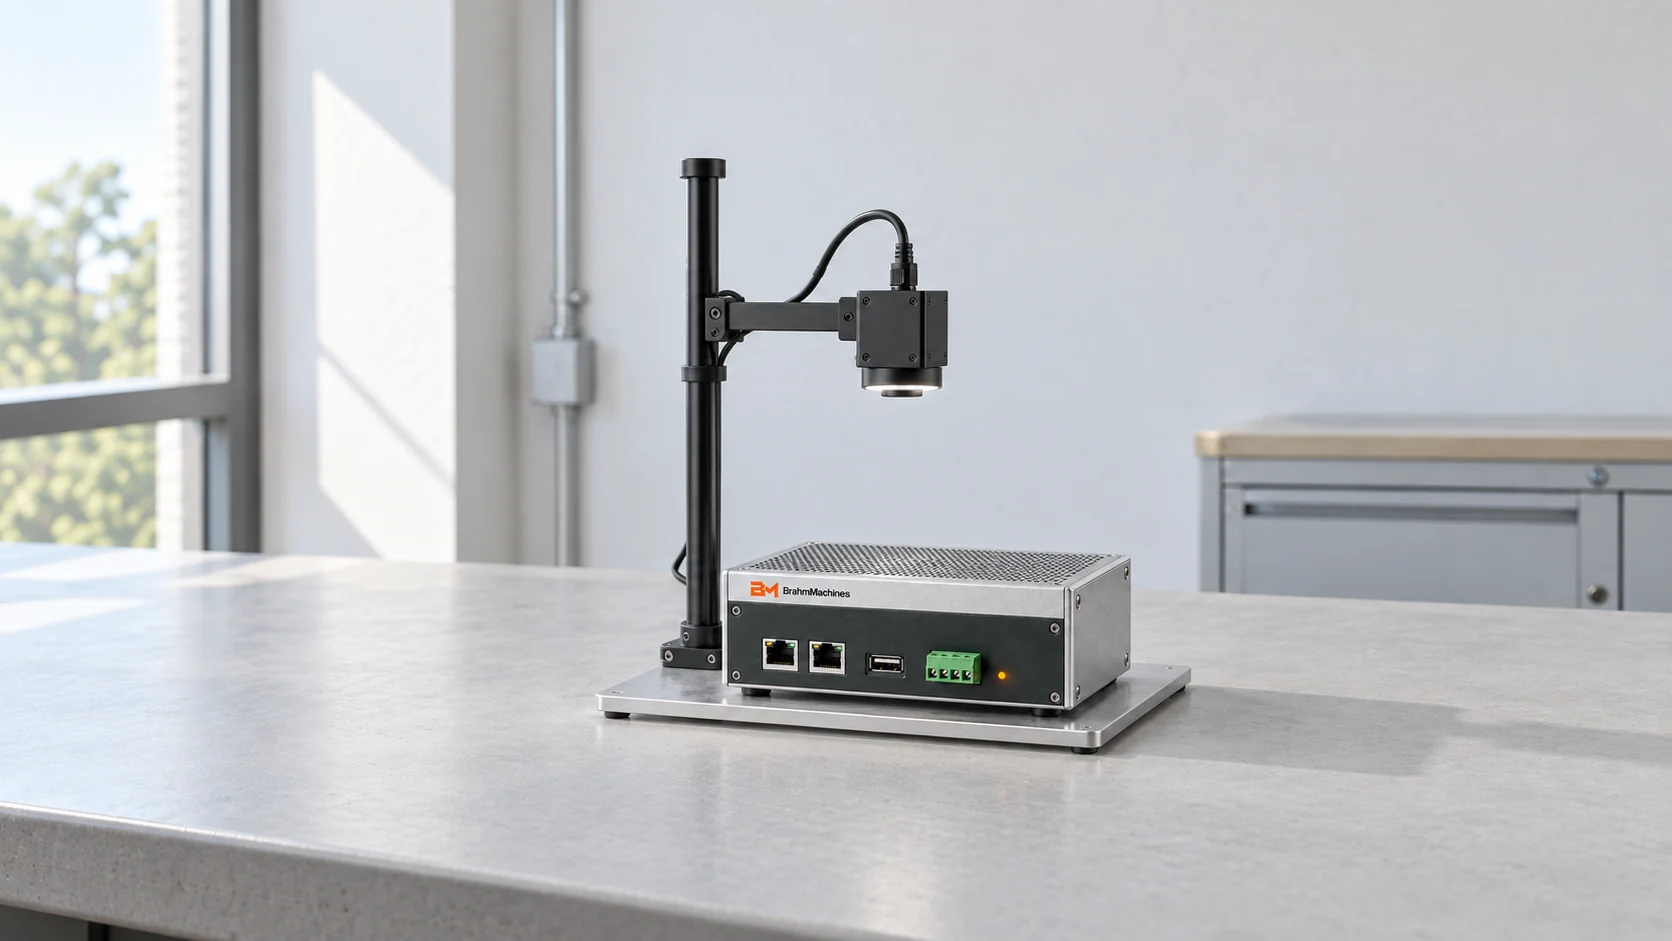 INSPECT / CONCEPT VISUALISATION
Inspect,
with context.
Defined presence and orientation checks
Label and identity verification
Inspection evidence attached to the unit
What comes in.
A repeatably located product and a validated inspection recipe.
What carries forward.
An inspection result for the specific checks agreed in the pilot.
Prove the operation.
Then scale it.
Detection performance must be validated against representative defects. Vision is not a blanket quality guarantee.
Fixture design, cycle sequence, safety measures and acceptance criteria need to be agreed and validated for the actual application.
Back to all six cellsQuestions before the pilot
Can vision inspection replace all other testing?
No. A defined visual check can assess agreed features such as presence, orientation or label identity. It does not establish every electrical function or hidden condition. Representative defects and acceptance criteria are needed to validate each inspection.
Plan this step in the full build.
See the electronics pilot production scope, prepare the readiness checklist and define the functional test plan.
What are you
building next?
Bring the working electronics.
Let's define the process around them.